
Fluid handling is an important part of many industrial operations. Factories, workshops, chemical units, and processing plants often move liquids from one container to another. Manual handling can be slow, messy, and unsafe. Therefore, industries use specialized equipment for better control.
A Drum Pump provides a practical solution for transferring liquids from drums and containers. It helps operators move fluids with less effort and better accuracy. Moreover, the right pump can reduce spills and improve workplace efficiency.
Malhar Pump offers pumping solutions designed for different industrial fluid-handling needs. However, choosing the right equipment requires an understanding of the liquid, container, flow requirement, and operating conditions.
What Is a Drum Pump?
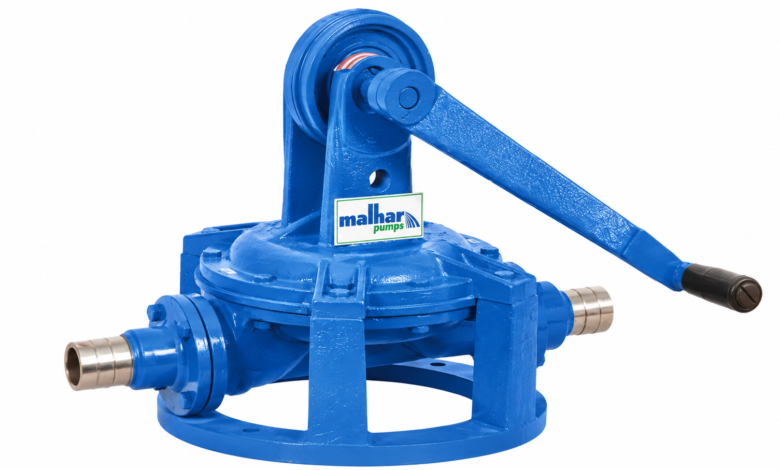
A Drum Pump is a compact pumping device designed to transfer liquids from drums, barrels, and similar containers. It usually fits through the opening of a drum. The pump then moves the liquid through a discharge pipe or hose.
These pumps are useful when large containers cannot be tilted easily. They also reduce the need for manual pouring. As a result, workers can handle liquids more conveniently.
Depending on the application, pumps can work with different liquids. These may include oils, solvents, chemicals, cleaning fluids, and other industrial liquids.
How Does It Work?
The basic operation is simple. First, the pump tube enters the drum opening. Next, the operator activates the pumping mechanism. The liquid then moves through the internal tube and exits through the outlet.
Different models use different operating methods. Some use electric power, while others use air pressure or manual operation. Therefore, industries can select a design based on their working environment.
Key Benefits of Using a Drum Pump
A well-selected Drum Pump can improve both productivity and handling safety. It also makes repetitive fluid transfer easier for workers.
1. Easier Liquid Transfer
Manual pouring requires physical effort and careful handling. A pump reduces this workload. Operators can transfer liquids without repeatedly lifting or tilting heavy containers.
This advantage becomes more important in busy industrial facilities. Regular pumping tasks can become faster and more consistent.
2. Better Workplace Safety
Some industrial liquids can cause irritation, burns, or other hazards. Direct handling can increase the chance of accidental exposure.
A suitable pump keeps the operator farther away from the liquid. Additionally, controlled transfer can reduce splashing and unnecessary spills.
3. Reduced Product Waste
Liquid can remain inside a drum after manual pouring. A suitable pumping system can help recover more usable material.
Therefore, businesses can reduce unnecessary product loss. This benefit can become significant when handling expensive industrial fluids.
4. Improved Operational Efficiency
Time matters in manufacturing and processing environments. A reliable pump can simplify repetitive transfer operations.
Operators can connect the system and transfer the required quantity efficiently. Consequently, teams can spend less time on basic material-handling tasks.
Choosing the Right Drum Pump for Your Application
Not every pump is suitable for every liquid. The selection process should begin with the application rather than the pump alone.
Consider the Liquid Type
First, identify the liquid being transferred. Its viscosity, temperature, chemical properties, and density can affect pump selection.
For example, a thin liquid may require different pumping characteristics than a thick oil. Similarly, corrosive chemicals may require special materials.
Check the Required Flow Rate
The required flow rate also matters. Some operations need quick transfer, while others require controlled and slower delivery.
Therefore, determine how much liquid must move within a specific period. This information helps narrow down suitable pump options.
Consider Material Compatibility
The pump materials should match the liquid being handled. Incompatible materials can lead to corrosion, contamination, or premature component failure.
For this reason, check the construction material before purchasing industrial pumping equipment.
Review Operating Conditions
The workplace environment can also influence your choice. Consider power availability, drum size, temperature, operating frequency, and installation requirements.
If the equipment will operate frequently, durability should receive special attention. A suitable industrial pump should support the required workload without unnecessary maintenance.
Common Applications of Drum Pumps
A Drum Pump can support many industrial and commercial applications. Its flexible design makes it useful wherever liquids need controlled transfer.
Chemical Industries
Chemical plants often handle liquids that require careful movement. Pumps can help transfer chemicals from storage drums into processing equipment or smaller containers.
Material compatibility remains essential in these applications. Operators should always follow the manufacturer’s recommendations.
Lubricant and Oil Handling
Workshops and manufacturing units frequently use oils, lubricants, and related fluids. Pumping systems can simplify transfer from large drums.
As a result, workers can reduce manual lifting and improve handling consistency.
Manufacturing Facilities
Manufacturing operations may use cleaning solutions, additives, coatings, and other liquids. A suitable pump can support regular material-transfer activities.
Moreover, controlled pumping can help maintain cleaner work areas.
Food and Processing Applications
Some processing environments require hygienic fluid transfer. In these cases, equipment must meet the required material and sanitation standards.
The pump design should match the specific application and industry requirements.
Best Practices for Drum Pump Operation
Proper operation helps improve equipment life and workplace safety. Before starting, inspect the pump and connections for visible damage.
Always confirm that the pump material suits the liquid. Also, secure the hose and outlet before beginning the transfer process.
Avoid running equipment outside its recommended operating conditions. Furthermore, clean the pump according to the manufacturer’s instructions after use.
Regular inspection can identify worn seals, damaged hoses, or other issues early. This simple practice can prevent unexpected downtime.
Malhar Pump focuses on practical pumping solutions for industrial applications. Businesses should still evaluate their individual requirements before selecting any model.
Frequently Asked Questions (5 FAQs)
1. What is a Drum Pump used for?
A Drum Pump is used to transfer liquids from drums, barrels, and similar containers. It reduces manual handling and provides controlled liquid movement.
2. Can a Drum Pump handle chemicals?
Yes, certain pumps can handle chemicals. However, the pump construction must be compatible with the specific chemical being transferred.
3. Are Drum Pumps available in different operating types?
Yes. Depending on the application, users can find manual, electric, and air-operated designs. The correct option depends on the required flow and workplace conditions.
4. How do I choose the right Drum Pump?
Consider the liquid type, viscosity, temperature, required flow rate, container size, and material compatibility. Operating conditions should also influence the selection.
5. How can I maintain a Drum Pump?
Inspect the pump regularly and keep its components clean. Check seals, hoses, and connections for wear. Follow the manufacturer’s maintenance instructions for better performance.
Conclusion
A Drum Pump can make industrial liquid transfer faster, safer, and more convenient. It reduces manual effort while helping operators maintain better control during pumping operations.
However, the right selection depends on the liquid, flow requirement, materials, and working environment. Therefore, businesses should evaluate these factors before choosing equipment.
With suitable equipment and proper operating practices, industries can improve fluid-handling efficiency and reduce unnecessary waste. If you need a reliable solution for your application, consult Malhar Pump to discuss your specific pumping requirements.